Create a code-to-duty allocation
List product code, ionic family, form, qualified plant and application, quantity and preparation standard. Keep separate approvals for anionic, cationic or nonionic duties.
Do not assume that one successful slurry or sludge trial authorizes another plant's use. Even two plants buying the same family can have different preparation capacity and separator endpoints.
Keep the quotation itemized
Request code-specific quantity, specification, packaging and price basis. Clarify common freight or handling costs without hiding which material is being supplied.
If the factory proposes consolidation through a substitute code, review the technical consequence explicitly. Commercial convenience alone does not establish that one grade can replace several accepted products.
Preserve packages and documents
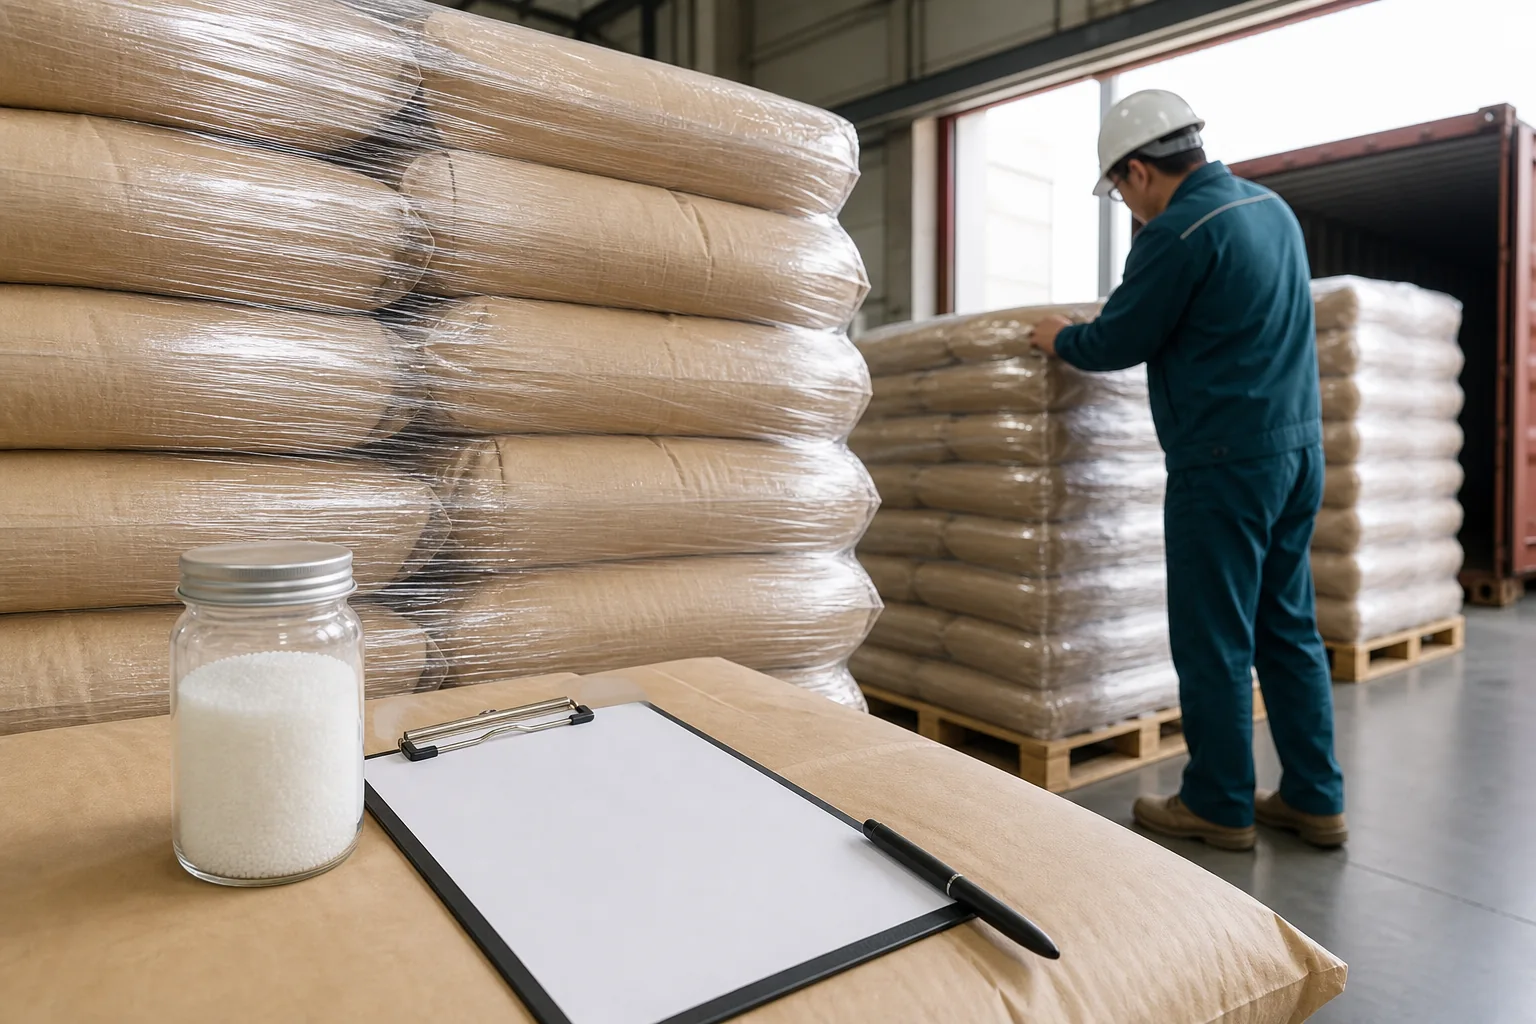
Agree labels that remain clear when pallets are separated. Map unit or pallet groups to code, batch, net contents and intended receiving destination.
Keep lot documents associated with the appropriate shipment lines. A combined packing list should support segregation rather than require operators to infer identity from appearance or bag color.
Prepare receiving and internal transfer
Have each receiving plant confirm storage, handling and document requirements. Define who checks allocation before material enters the preparation area.
The packaging handover supports this process. Record any later transfer to another facility as a controlled allocation change, with the receiving plant's technical approval.
A consolidated-order release sheet
Reconcile ordered quantity, package count, batch documents and destination for every code. Keep analytical acceptance and application approval separate, marking untested plant uses as pending.
Send the allocation through the multi-grade PAM factory enquiry. Ask which consolidation options can be offered for the actual order. No combined-order discount, shared MOQ or universal interchangeability is implied without a code-specific written proposal.
Allocation release evidence
| Checkpoint | Evidence to retain | Decision boundary |
|---|---|---|
| Duty | Map each code, ionic family, form and quantity to the plant and application that actually approved it. | One successful trial cannot silently qualify every receiving plant or another family's duty. |
| Packages | Keep pallet or unit references, net contents and lot documents linked to the correct order line. | Bag color, powder appearance or an overall shipment total cannot replace positive grade identification. |
| Transfer | Confirm each receiving facility's storage, preparation and release requirements, including later internal reallocations. | A consolidated order does not establish universal interchangeability, a shared MOQ or a promised combined-order discount. |